21
Oct
Solar Mounting Structure Base Plates: Types, Design and Selection Guide
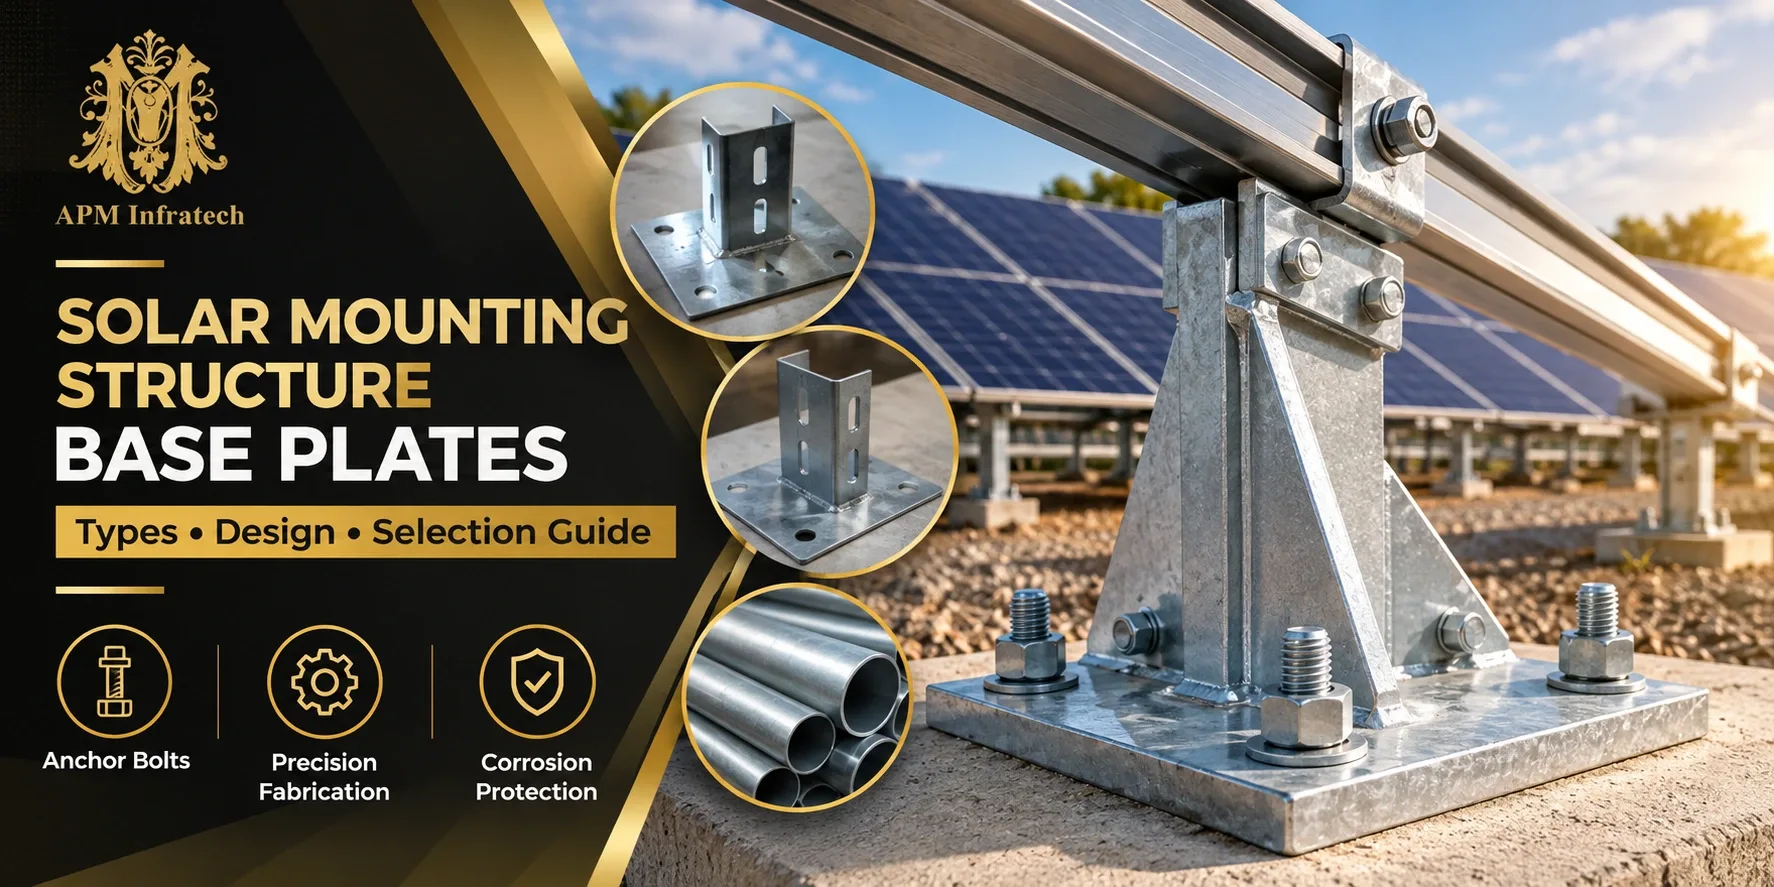
A solar mounting structure base plate is the steel interface that transfers column or post forces into concrete, steelwork or another approved support. It is not a generic flat plate selected only by length and thickness. Plate dimensions, steel grade, hole pattern, weld detail, anchor arrangement, corrosion protection, grout, edge distance and installation tolerance must come from the structural load path and the verified site condition.
For procurement, freeze the approved drawing before requesting comparable prices. State whether the requirement is a cast-in anchor plate, post-installed anchor plate, welded steel interface or adjustable assembly. APM Infratech lists a hot-dip solar base plate within its solar-structure range; the project engineer should still approve every dimension, coating, anchor and weld for the actual installation.
Why the Base Plate Is a Critical Structural Interface
Wind uplift, overturning, shear, dead load and installation eccentricity converge at the base connection. A plate that looks substantial can still fail its purpose if the anchors are too close to an edge, the weld is incomplete, the concrete is weak, the grout is missing or the column lands outside the designed footprint. The plate, post, weld, anchors, grout and supporting substrate therefore have to be checked as one connection.
The connection also determines whether the structure can be aligned without forcing members into position. Poor tolerances can twist columns, misalign purlins and create local stresses before the modules are installed. A small saving on plate fabrication can lead to drilling, rework, damaged galvanizing or delayed erection. Treat base-plate information as controlled design data rather than a site-adjustable detail.
| Base-plate input | Why it matters | Evidence to request |
|---|---|---|
| Design actions | Sets bending, shear, uplift and bearing demand | Signed calculation or connection schedule |
| Support condition | Controls anchors, grout and edge checks | Foundation or steel-support drawing |
| Plate and steel grade | Controls strength and stiffness | Material certificate |
| Hole and anchor pattern | Controls fit and concrete capacity | Fabrication drawing and template |
| Coating system | Controls corrosion durability | Process certificate and inspection |
| Site tolerances | Controls erection and alignment | Survey and inspection record |
Common Base-Plate Types and Where They Fit
A conventional fixed plate has drilled or punched holes and a welded post, usually paired with cast-in or post-installed anchors. Slotted plates provide limited adjustment but need correctly designed washers and slip control. Stiffened plates use ribs where the plate would otherwise bend excessively. A welded interface can connect a solar post to existing structural steel, subject to the parent member and fire or coating requirements.
Adjustability should solve a defined tolerance problem, not hide an uncertain foundation layout. Oversized holes, field-cut slots and stacked washers can reduce capacity or bearing area. If a proprietary bracket or channel is proposed, request its tested or calculated capacity, compatible fasteners and installation limits. No type is universally best; the correct choice follows the substrate, loads, erection sequence and access.
Loads That Must Reach the Foundation
The engineer should determine design actions for each support location, including wind pressure and suction, dead load, maintenance load, seismic effects where relevant and any snow or environmental load in the project basis. Edge, corner and internal supports may have different forces. Using one plate everywhere may simplify fabrication, but it should be justified by the governing demand rather than assumed.
Load combinations and safety factors belong to the applicable design framework and project specification. The plate must be checked for bending, bearing, shear and local effects; anchors for tension, shear, interaction, spacing and edge distance; concrete for breakout or pull-out; and welds for the transferred forces. A catalogue plate cannot guarantee performance without this connection-level verification.
Plate Dimensions, Thickness and Stiffeners
Plan dimensions must provide enough bearing area and space for anchors, tools, washers and welds while respecting concrete edges. Thickness controls plate bending between the column, anchors and bearing region. A larger plate is not automatically safer if its anchors remain poorly positioned, and a thick plate does not compensate for an inadequate weld or weak substrate.
Stiffeners can reduce local plate bending or strengthen the post junction, but they change welding, galvanizing drainage and access for tightening. Show their size, orientation, welds and clearances on the drawing. Define flatness and permissible distortion after welding and coating. Fabricators should not add or omit stiffeners based on workshop convenience without an approved revision.
Steel Grade and Material Traceability
Specify the steel grade for the plate, column, stiffeners and washers rather than using only the word mild steel. The required yield strength, weldability and thickness tolerance should match the structural design and purchase standard. Mixed or unidentified material makes calculation assumptions difficult to verify and weakens quality control across a large solar project.
Request certificates tied to heat or batch identification where the project requires traceability. Verify plate thickness, dimensions and markings during receipt inspection. APM Infratech presents MS solar mounting structures and a broader solar structure portfolio use those pages to understand the offered categories, then make the purchase schedule control the exact project material.
Anchor Bolts and Concrete Compatibility
Cast-in anchors offer controlled embedment when foundations are poured around an accurate template. Post-installed anchors can suit retrofits, but their type, diameter, embedment, drilling, cleaning, adhesive or expansion mechanism and installation conditions must follow an approved design and manufacturer instructions. Reinforcement, edge distance, concrete strength and cracked-concrete assumptions can change capacity.
Do not move an anchor to avoid reinforcement without engineering review. Site-drilled holes should be surveyed and scanned where needed, and installers should record drill diameter, depth, cleaning and torque or cure requirements. The anchor specification must also address material and corrosion exposure. A galvanized plate paired with an unsuitable buried or wet-zone fastener can create an early maintenance problem.
Hole Patterns, Slots and Tolerance Control
Hole centres, diameter, slot orientation and permitted positional tolerance should appear on a fabrication drawing. The anchor template must use the same controlled geometry. Slotted holes may permit movement in one direction, but they require adequate plate edge distance and a washer or cover plate capable of transferring the designed force. Free site adjustment in two directions should not be created by torch cutting.
Survey foundations before delivery and compare actual anchor coordinates with the erection tolerance. Where deviations exceed the approved range, obtain a designed repair. Heating, bending, cutting or welding anchors on site can damage material and invalidate capacity. The fastest installation is achieved through templates and surveys, not through loosely defined holes.
Welding Details and Fabrication Quality
Show weld type, size, length, continuity and inspection requirement. The joint between post and plate may include fillet welds, full-penetration details or stiffeners depending on forces and geometry. Access, start-stop locations and distortion control matter. Welding procedure, consumables and welder qualification should match the project requirements and steel grade.
Inspect fit-up, root condition where relevant, weld profile and visible defects before coating. Non-destructive testing should follow the approved inspection plan rather than a generic promise. Grinding should not reduce the effective weld or plate thickness. After repair, restore the specified corrosion-protection system using an approved method and record the location.
Hot-Dip Galvanizing and Other Corrosion Protection
Hot-dip galvanizing can protect exposed steel, but coating durability depends on surface preparation, steel chemistry, drainage, venting, thickness and handling. Fabrication should be complete before galvanizing wherever practical. Closed cavities, overlapping plates and poorly placed holes can create process hazards or uncoated areas. The drawing should include vent and drain provisions where needed.
Specify the governing coating requirement and inspection method. Check appearance, coverage, thickness and damage at contact points and edges. Threads may require compatible treatment and allowances. APM also lists hot-dip galvanized solar structures and GI solar structures the final coating choice should follow exposure, design life, maintenance and project specifications.
Grout, Bearing and Leveling
Where a steel plate bears on concrete, the design may require non-shrink grout to provide uniform support and transfer compression. Leveling nuts or shims used during erection are not automatically a permanent bearing system. Define grout type, gap, edge formwork, substrate preparation, placement and cure. Voids beneath the plate can concentrate stresses and retain water.
Set the plate to the required elevation and slope before grouting, then protect the work from movement and premature loading. Confirm whether the design permits leveling nuts below the plate and how they affect anchor forces. Inspect grout continuity and finish. Seal or drainage details should prevent persistent moisture without trapping water against the post.
Rooftop, Ground-Mount and Steel-Deck Differences
A ground-mounted plate often connects to a concrete pedestal or pile cap, while a rooftop plate may connect to reinforced concrete, structural steel or a roofing support. Roof waterproofing, insulation, drainage and thermal movement add interfaces that do not exist in open ground. Penetrations must be coordinated with the roof-system provider and structural engineer.
Thin roof sheets are generally not foundations unless the complete system is designed and approved for that load path. On existing buildings, verify member capacity, corrosion, access and as-built geometry before fabrication. Ground sites need survey control, concrete quality and elevation management. Do not copy one base-plate detail between these applications without review.
Procurement Schedule and Quotation Comparison
Issue a plate schedule listing mark number, quantity, plate dimensions, thickness, steel grade, post size, stiffeners, welds, hole pattern, coating, anchors, washers and documentation. Separate supply-only, anchor supply, template, grout and installation scope. Ask bidders to identify exclusions and deviations instead of using “as per drawing” when the drawing remains incomplete.
Normalize quotes against the same bill of materials. Check whether unit weight, scrap, galvanizing, testing, packing, transport and site touch-up are included. Very low pricing may reflect thinner plate, different steel, incomplete coating or omitted anchors. Commercial comparison should begin only after technical compliance and traceability are clear.
| Quotation item | Minimum clarification | Acceptance evidence |
|---|---|---|
| Plate assembly | Dimensions, thickness, grade and mark | Drawing and dimensional report |
| Welded post/stiffeners | Weld detail and inspection | Weld record |
| Anchors and washers | Type, grade, coating and template | Certificates and installation record |
| Galvanizing/coating | Standard, thickness and repair | Inspection certificate |
| Packing and transport | Protection against distortion and abrasion | Delivery inspection |
| Site installation | Survey, grout, torque and handover | ITP and as-built record |
Installation Sequence and Hold Points
Begin with approved drawings, foundation release and survey benchmarks. Inspect anchor templates before concrete, then re-survey anchors after the pour. Match plate mark numbers to locations, clean bearing surfaces, set elevation and alignment, install washers and nuts in the specified sequence, grout where required and apply final tightening or torque only under the approved method.
Use hold points before concealed work, grouting and module loading. Record elevation, plumb, anchor engagement, nut position, coating damage and grout condition. Site modifications require a written disposition. For large arrays, a trial installation can confirm templates, tools, access and tolerances before mass production continues.
Inspection and Quality Documents
A practical inspection plan covers incoming steel, cutting, drilling, dimensional fit-up, welding, pre-coating release, coating, packing, receipt, erection and final survey. Define sampling and acceptance criteria. Check that holes remain clear after coating, plates are not warped, weld spatter is removed and identification remains legible.
Handover should include approved drawings, calculations or connection schedule, material and coating certificates, weld and inspection records, anchor installation data, grout batch information, survey results, nonconformance closures and as-built photographs. Documentation is especially valuable when a future repowering, module change or structural audit must understand the original connection.
Frequent Base-Plate Mistakes to Avoid
Common errors include selecting by plate thickness alone, copying hole patterns without checking anchors, using field-cut slots, ignoring concrete edges, welding after galvanizing without proper repair, stacking loose washers, omitting grout and accepting bent anchors. Another mistake is assuming every support sees the same load when edge and corner zones can govern.
Avoid promising a universal load capacity for a loose base plate. Capacity belongs to the complete connection and substrate. Also avoid treating coating colour as proof of galvanizing quality. Require measurable specifications, controlled drawings and evidence at each hold point. These steps reduce installation disputes and provide a defensible technical comparison.
Manage Nonconformances Without Improvised Repairs
Typical nonconformances include misplaced anchors, warped plates, blocked holes, insufficient thread projection, coating damage, poor grout or a column that cannot be aligned within tolerance. Quarantine the affected location, record dimensions and photographs, and compare the condition with the approved drawing. Do not enlarge holes, cut plate edges, bend anchors or add packers simply to maintain erection progress.
The responsible engineer should issue a repair or use-as-is disposition supported by the actual loads and substrate. The solution may require a designed cover plate, approved post-installed anchor, grout replacement, local coating restoration or component remanufacture. Inspect the completed repair and update the as-built record. A controlled repair can preserve capacity; an undocumented convenience fix leaves future reviewers without a reliable load path.
A Base-Plate Enquiry Checklist
Send the array layout, post and member sizes, design reactions, support drawings, concrete data, anchor preference, plate schedule, coating requirement, environment, site location and programme. State whether engineering review, shop drawings, anchors, templates, grout, erection and testing are included. Add packing and identification requirements for multi-block projects.
Request a compliance statement, deviation list, material and coating evidence, manufacturing lead time and inspection plan. APM Infratech explains its broader engineering background on the About Us page. Treat current certifications, capacity, warranty, prices and delivery as quotation-specific items that must be verified in writing.
Frequently Asked Questions
1. What is a solar mounting structure base plate?
It is the structural steel interface that transfers forces from a mounting post or column into an approved foundation or supporting member.
2. How is base-plate thickness selected?
Thickness is calculated from plate bending, bearing, anchor forces, post geometry and design loads; it should not be selected from a generic table alone.
3. Are slotted holes acceptable?
They can be when deliberately designed with adequate edge distance, bearing and washer details. Site-cut slots are not an automatic tolerance solution.
4. Should anchors be cast in or post installed?
Either may be suitable. The choice depends on construction stage, concrete, loads, edge distances, installation control and the approved anchor design.
5. Why is grout used below a base plate?
Specified grout provides uniform bearing, fills the designed gap and transfers compression. Its need and thickness come from the connection detail.
6. Can a base plate be welded after galvanizing?
Only under an approved repair procedure. Welding damages the coating and may require safety controls, inspection and restoration.
7. Does hot-dip galvanizing prevent all corrosion?
No. It improves protection, but durability still depends on coating quality, exposure, drainage, damage, fastener compatibility and maintenance.
8. What tolerances should be checked?
Anchor location, hole pattern, plate flatness, elevation, post plumb, member alignment and foundation coordinates should match the approved project tolerance.
9. Can one base plate be used at every array position?
Possibly, if designed for the governing actions and compatible with all supports. Edge, corner and internal positions may have different demands.
10. What should be inspected before dispatch?
Verify material, dimensions, holes, identification, welds, distortion, coating, threads and packing against the approved drawing and inspection plan.
11. What information is needed for a quotation?
Provide drawings, quantities, steel grades, loads or connection schedule, anchors, coating, inspection, packing, location and installation scope.
12. Who approves a base-plate change on site?
The responsible structural engineer or authorised project designer should assess and approve the change before work continues.
Secure the Array by Getting the Foundation Interface Right
A reliable solar support begins where the column meets the foundation. Freeze reactions, substrate data, anchors, plate geometry, welds, coating and tolerances before ordering, then inspect the connection through fabrication and installation. Review APM Infratech’s solar structure range and use its contact page to request a drawing-based base-plate proposal with project quantities, site conditions, coating, anchor scope and delivery requirements.